

OEM performance engines. Tailor designed and manufactured for your supercar, race car, and marine use case!
Kirkkonummi, Finland
Joined January 2013
- Tweets746
- Following66
- Followers274
- Likes483


First two customer 4000hp billet 5-axis CNC Hel engines in final assembly!
Valve clearances in spec with custom cams, cam drive setup ok, covers have all o-rings correct, water pump, dry sump oil pump mounting and drive, custom vibration damper mount, custom billet crank with bearing clearances to spec, custom billet titanium connecting rods with clearances and piston pin in check, and many more details!
Everything takes 10x as long to assemble the first time when we double check what needs to be measured, what our measurement accuracy is, document everything correctly, and mark the custom tooling correctly and make instructions for how to use them.
Hopefully in the final stretch now!
Soon to go into a couple of absolutely mental r35 GT-R's, in place of the nissan vr38dett engines.
And we will see how close to the designed 4000hp they will get! (Or exceed!)


Extreme design criteria is how we would sum up the staring point for the design on our Hel connecting rods.
Billet Titanium CNC. 4000hp for 6 rods.
To keep the piston pin and its bearing alive as long as possible, it's very important for the connecting rod small end to flex the right amount (about as much as the piston pin) during high load. This is easier to do, the lower your material modulus of elasticity is.
Aluminum would be the go to material, but for the load capacity we needed we didn't have enough space available.
Iron alloy (steel etc) would be one option, but its high stiffness causes design issues when design in the correct amount of flex.
Luckily there was just barely enough space available in the tight piston and crankcase housing clearance to go with titanium.
Yes it's more difficult to machine. But we 5-axis CNC mill stainless steel merge collects. Titanium was not going to be a problem.
Pushing a design this hard requires looking at each load case individually and look at the relevant ultimate strength and fatigue properties.
The piston pin bore experiences a confined compressive pressure during combustion. Depending on design geometry this can be treated as a non fatiguing load case.
How the small end pin bearing area flexes is extremely important. This is a section where we design wise had to push multiple iterations to get the strength high enough, keep flex exactly right, and keep minimum radius is check for manufacturing. Ultimately we were just barely able to make this work. But we are happy with the design, and it should have a good chance of holding our design power.
The overlap load at max rpm on the other hand causes a tensile load on the small end. This requires load optimization to stay under the anticipated fatigue load for the material.
Big end has a completely separate design criteria. Stiffness. It needs to be stiff enough to keep the big end bearing round enough, to then in turn keep the oil film in the big end bearing in shape. Ultimate stress is as a result relatively low in the big end section. Depending on design. We've removed as much material as possible while still keeping the big end stiff. We implemented a I-beam type cross section in the bottom half of the big end (high stiffness, low mass) to optimize this. The top half of the big end has cut-outs to reduce mass on the neutral axis (in relation to bearing stiffness), while maintaining full width stiffeners to distribute compressive loads evenly.
Custom racing bearings. Not ideal, but the engine calls for a very large crankshaft pin diameter to keep the crank alive. So rods and bearings just have to adapt.


Now free shipping for all orders over 200€ from our webshop! Especially good for billet merge collector orders.
shop.elmerracing.com
4000hp Hel engine finally assembled!
'Bolt-in' replacement for the nissan gt-r r35 vr38dett engine. But 5000cc and designed for 4000hp.
Pre-order price still available till 30.6.2026 after which it will be bumped due to the engine needing billet titanium rods, and a few other expensive components.
4000hp Hel shorblock test assembly finished, in spec.
Manual clearanced block to fit slightly beefier billet titanium rods. CAD fix for batch 2. Structurally ok though, approved for customer use.
Long block getting ready to go together also! First fully assembled head.


Introducing our Billet Merge Collector 'What could go wrong?' durability guarantee!
1 free replacement, regardless of how it broke. Just send us the pictures/videos and permission to use them. Full terms on the TOS page on our webshop.
So what happened in this customers case?
Based off the images it looks like a combination of factors. Vibrations and thermal expansion loads from the wastegate exit pipe transmitting though the wastegate to the wastegate mounting. High temperatures due to thermal insulation and likely closed floor (time attack car) with minimal airflow around the exhaust. Sharp edge on the *inside* of the wastegate duct to the runners/turbo area. Lots of heat cycles and use.
Due to customer time constraints to get the car ready for the next event, we sent out a replacement collector of the same dimensions, but updated model with filleted wastegate exit (yellow highlight in picture, all our newer models have this update). Other option was to make a custom one from 316 or 321 stainless material, but this would have taken a few more days for raw material lead time.
We also recommended changing out the slip-over fitting for a flex piece. And incorporate a external support clamp between the wastegate and main exhaust pipe.
And if possible, any slight increase in airflow around the header pipe would help reduce peak temps and thermal cycle load.
We think our 5 axis Billet CNC Merge Collectors are the most durable parts available. But sometimes things can happen. If it does, we have your back. And will try to help you avoid another failure.


Could the 2031 F1 engine rule revamp be interesting for OEM race engine manufacturers like us?
Maybe!
F1 going to better regulations for 2030 or 2031?
Elmer Racing engines in F1 maybe?
Definitely would be interesting if the regulations are open enough.
Certainly enough time to build a department.

FIA president Mohammed Ben Sulayem says #F1 is going to V8s in 2031 regardless of what manufacturers want.
All they can do is approve an earlier switch:
the-race.com/formula-1/f1-v8…
4000hp v6 first engine assembly progress.
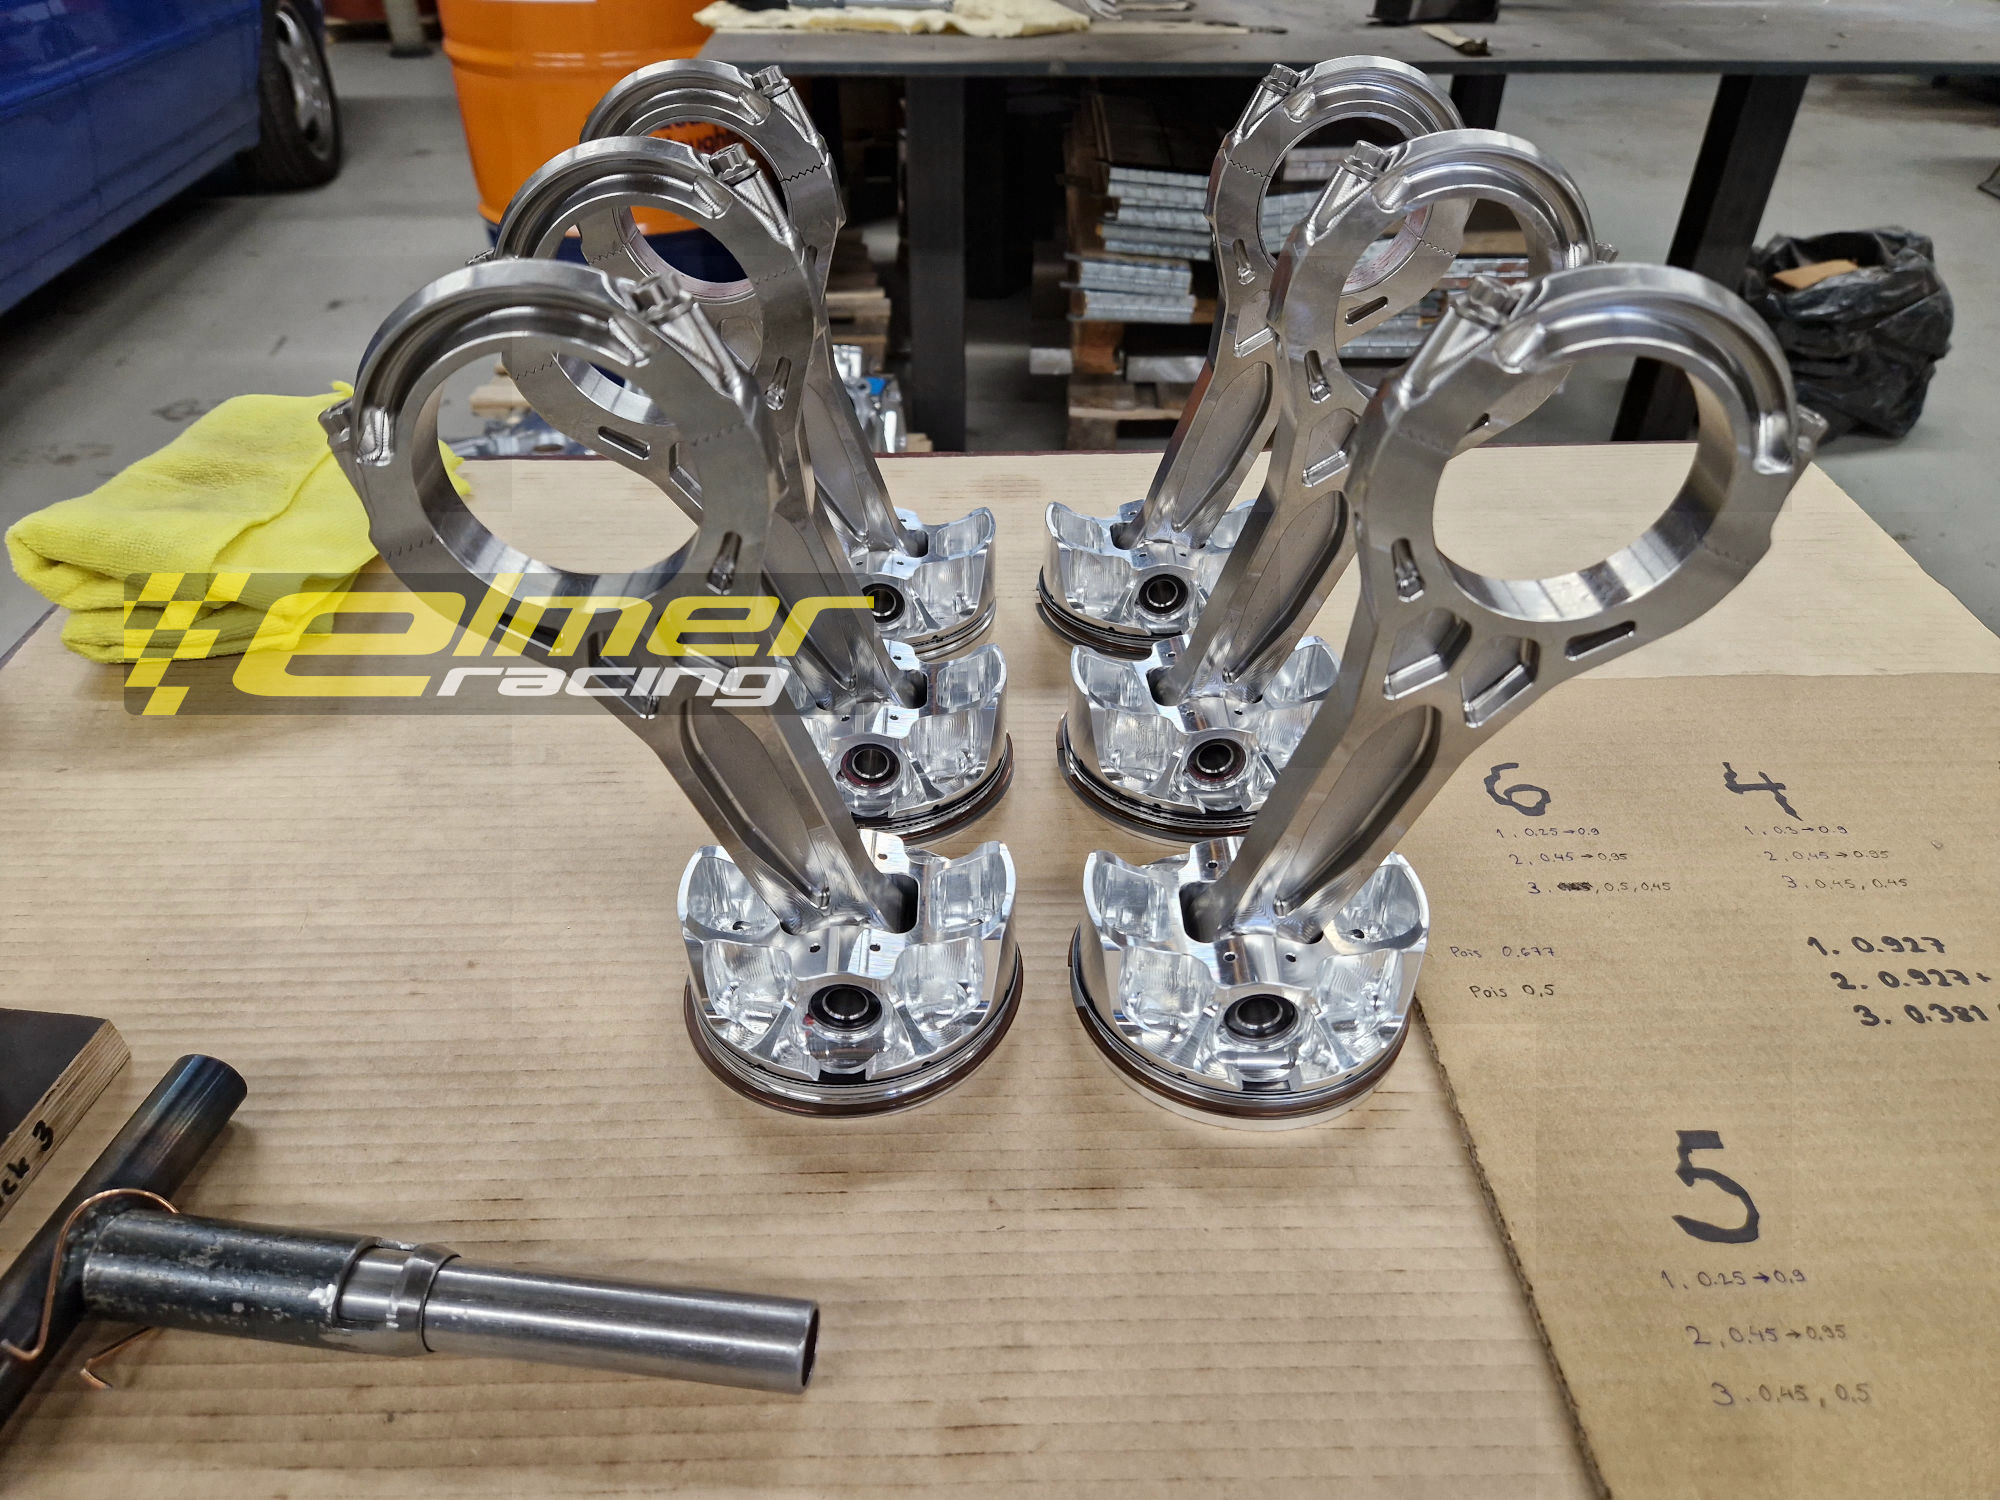
Rods, bushings, pins, clips, pistons, piston rings. All looking good. Tested for rotation clearance in the crank case earlier.
Custom tool to mount piston pin clips in the bottom left of the picture. Crazy stiff clips, hence the need for a tool, but should stay in there even at max rpm (well above 11,000rpm)!
CNC toolpath update for the 4000hp Hel billet tool steel crank looking mint!
No more small corners left over here and there. And much more reasonable tool wear.
Bearing surface polishing/grinding should be much faster and easier also.
The surface shape around the highest loaded areas is especially critical for longevity in a crankshaft being pushed as hard as this.
Peak stress needs to be kept in check, but for longevity it's even more important that the stress levels don't change too rapidly, as that aids crack propagation/fatigue.
This is why our crank designs have a almost organic shape. With the power density we push for in our designs there is no other way to make this work. Design time is crazy high (compared to basic cranks), but absolutely needed.
And the CNC machining side then needs to be able to effectively make these crazy shapes. This also takes a lot of skill and dedication to achieve.
The up side is that at least design criteria wise, we can push these crazy high power densities that are unheard of from other OEM's.
The only reason we even attempted this was how well our Thor crank has performed. Giving us confidence in that we at least know a little about what we're doing.
There are no guarantees in racing or when pushing boundaries. But it's what we love, and what we're good at.


2 Versions of our parallel entry 4-to-1 billet merge collectors now! Standard and the new lightweight.
We launched a new website!
Because that's what you do today!
42MW 43% efficiency in a 40' container
Datacenter ready.
elmerpower.com

Hel test assembly progress update!
All major components fit and are within tolerances. A few bolts need different spec heads, and waiting on a few smaller parts.
But we're getting closer to 4000hp.


Close up look at how hard the design is pushed on our 4000hp Hel engine.
Intake and exhaust valve guides are fully integrated into the port design. And the port cross section area fully takes this shape into account.
The exhaust value guides have a shorter external end taper and different internal diameter for the tip to reduce the temperature of the tip. But still needs to be very close to the valve head to get good heat conduction and valve cooling.
Intake side is fully contoured behind the valve guide hump to reduce turbulence.
At full power both the intake and exhaust flow is mach limited during the entire valve open period. Shapes and maintaining port cross section really matter to help reduce shock waves and port flow losses close to the valve.


